📍 Oman Chicken Slaughter Factory Refrigeration Project
Design, supply, installation, and commissioning of a complete multi-temperature-zone cold storage system for a modern chicken slaughtering and processing line, compliant with HACCP and local food safety standards.
Design Temperature Specifications
Chiller / Store Area
0 ~ +4°C
Our Solution
Faced with the critical requirements for food safety, processing efficiency, and energy management in modern poultry processing, we delivered a comprehensive, turnkey refrigeration solution that bridges precision engineering with flawless execution.
► Customized Precision Engineering
- From the initial phase, our engineering team developed detailed, custom refrigeration unit and system layout drawings specifically for this facility. Each drawing was meticulously crafted to align with the client's slaughter-to-freeze process flow, ensuring the designed parameters for each critical zone (0~4°C chilling, -18°C freezing, -40°C blast freezing) perfectly support the entire production chain.
► Quality-Assured Fabrication
- All equipment fabrication and piping prefabrication were executed based on client-approved precision drawings. This ensures every component meets exact specifications before leaving our factory, guaranteeing quality and simplifying on-site integration.
► On-Site Management
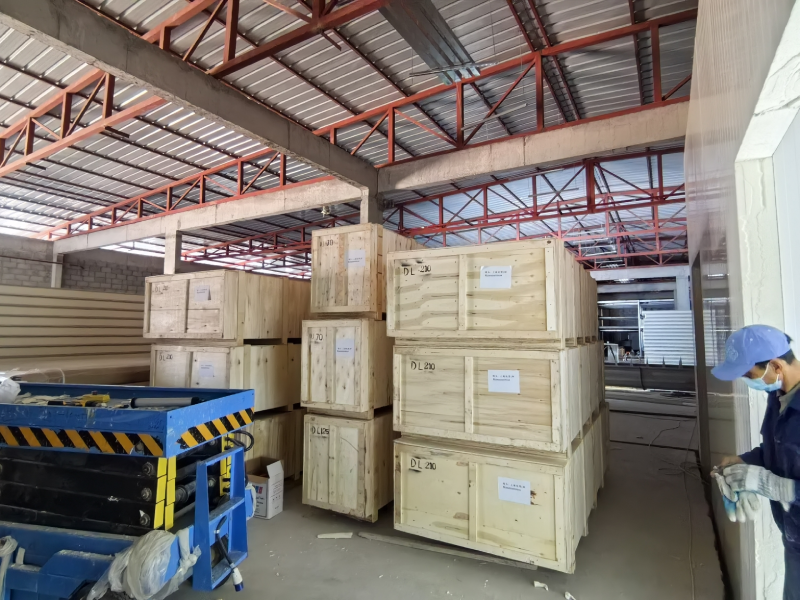
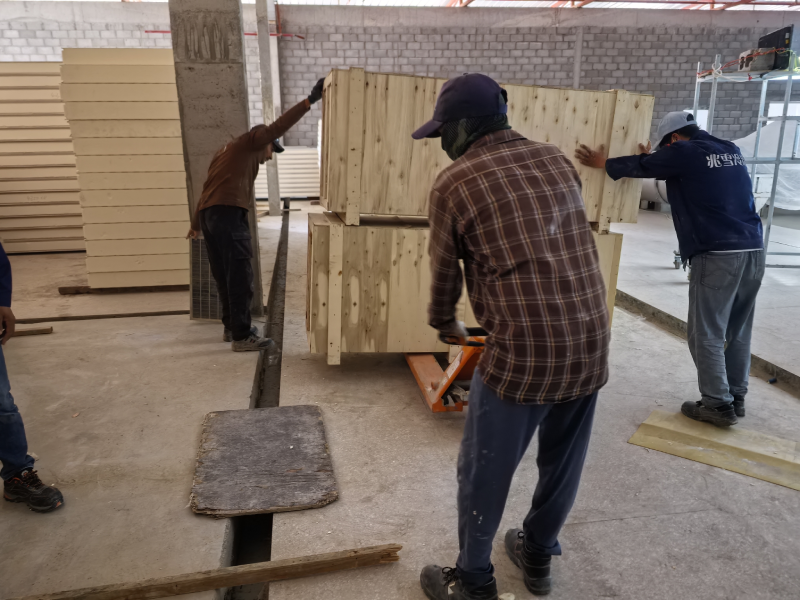
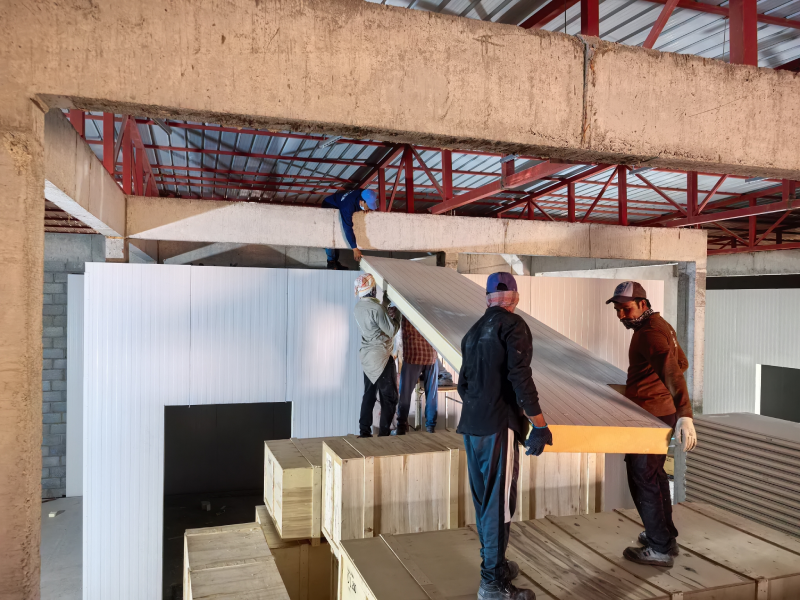
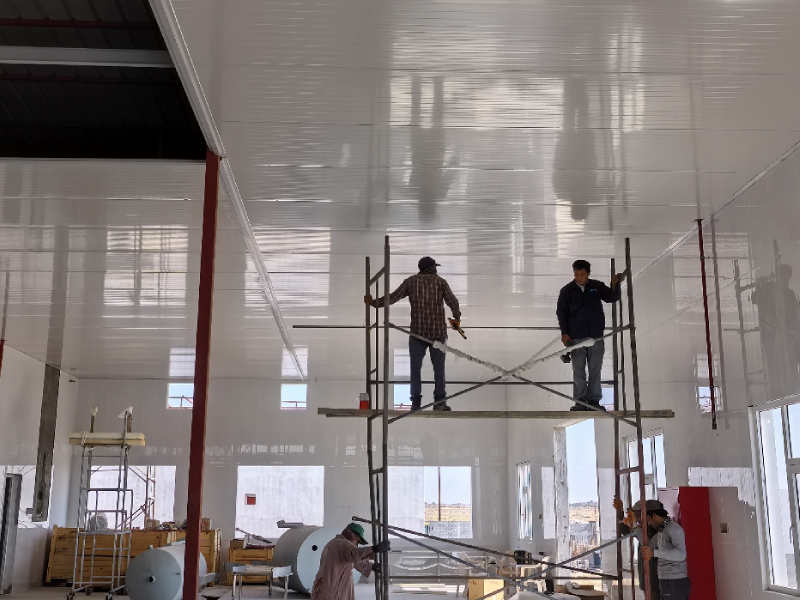
- The installation phase is led on-site in Oman by our certified project engineers. They provide direct technical supervision and work in close collaboration with the local workforce, ensuring all installation practices meet international standards and our stringent protocols. Currently, over 50% of the installation is complete as per our planned schedule, with system integration progressing smoothly.
Results
This project demonstrates the capability to integrate refrigeration systems that achieve high reliability and precise multi-zone temperature control under complex operating conditions.
✔ Ensures Superior Food Safety & Product Integrity The precise multi-zone temperature control, particularly the rapid pull-down capability of the -40°C blast freezer (designed to freeze product from +4°C to -18°C core temperature within 8 hours), drastically inhibits microbial growth. This rapidly locks in freshness, preserves nutritional value, and extends product shelf life, delivering safer, higher-quality chicken to the end consumer.
✔ Operational Reliability The integrated refrigeration solution is designed for continuous, stable operation of the processing line. The reliable blast freezing capacity directly increases batch processing speed and overall plant throughput, while the robust system design with equipment redundancy minimizes downtime risks.
✔ Efficient Handover Through drawing-based and standardized project management, along with efficient on-site collaboration, we completed the project on schedule. Post-commissioning performance tests confirmed all temperature zones operate within specified tolerances. The entire refrigeration system was put into operation as scheduled, meeting the designed performance indicators. The client reported a 15% increase in daily processing capacity post-installation.
 EN