📍 Philippines Banana Ripening Facility Project
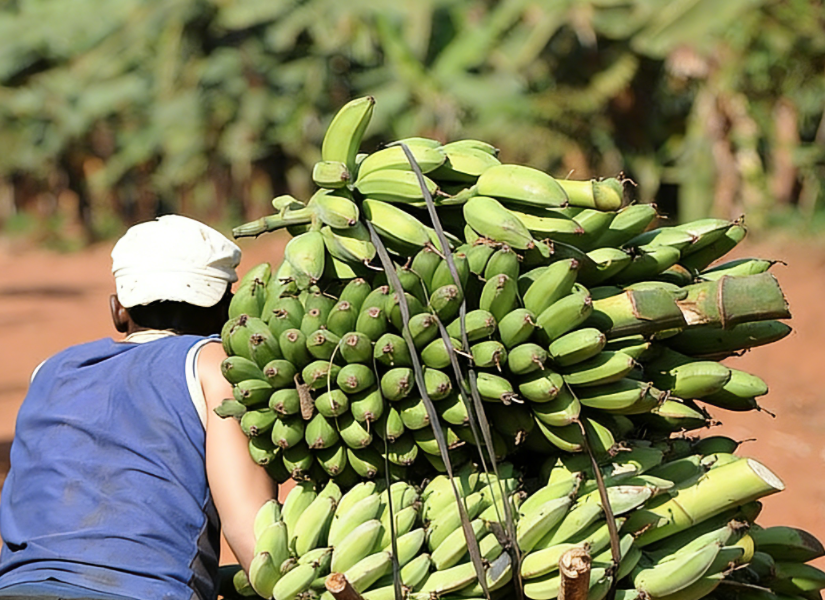
A major banana export and distribution company in the Philippines, specializing in supplying premium-grade bananas to domestic and international markets.
Initial Challenge
The client operated multiple banana ripening rooms with inconsistent temperature and ethylene gas control, leading to uneven ripening, excessive weight loss, and a high rate of product rejection. This resulted in significant product loss, unreliable supply schedules, and diminished brand reputation.
Core Objective
To design and implement a fully automated, precision-controlled ripening system that ensures uniform ripening, minimizes product loss, optimizes energy use, and provides complete traceability and control over the ripening process.
Our Solution
► Precision Multi-Zone Climate Control System
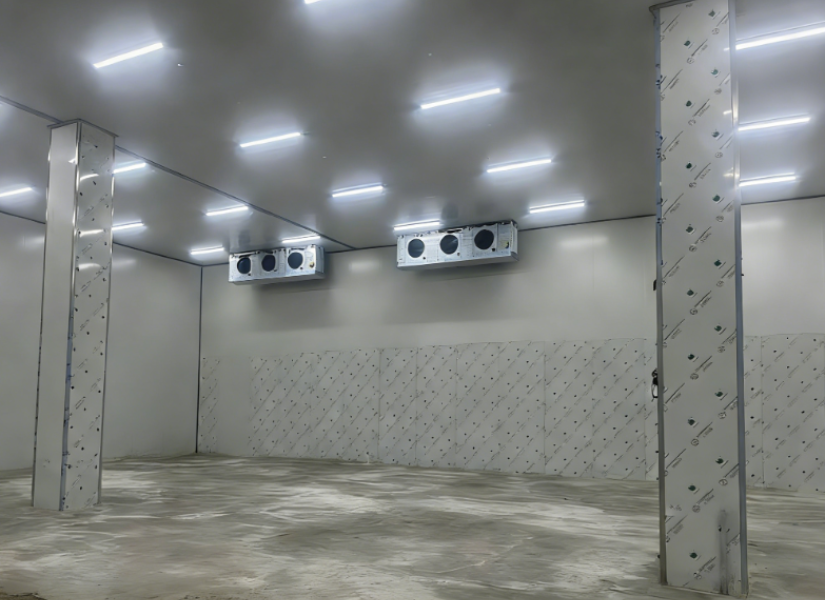
- We engineered and installed a dedicated, independent refrigeration system for each room with advanced multi-zone temperature and humidity control. Each ripening room is equipped with a high-humidity compatible air cooler and a humidification system. The system maintains the exact temperature profile (typically programmed from 13°C to 18°C in stages) and high relative humidity (88-92%, adjustable) critical for uniform ripening and minimizing moisture loss. Temperature uniformity within each room is maintained within ±0.8°C.
► Automated Ethylene Gas Injection & Ventilation Management
- The system features a fully automated, PLC-controlled ethylene gas injection, circulation, and exhaust system. It precisely administers ethylene from certified cylinders at programmed stages (typically 100-150 PPM) using mass flow controllers, followed by automated ventilation to remove CO₂ and residual ethylene. Gas concentration is monitored by electrochemical sensors. Safety features include gas leak detection and emergency purge ventilation.
► Centralized Monitoring & Data Logging Platform
- We provided a centralized, cloud-based monitoring and control platform. This allows operators to program, monitor in real-time, and adjust ripening cycles for all rooms from a single interface or mobile device. All critical data (temperature, humidity, ethylene/CO₂ levels, cycle timestamps) is automatically logged and stored for one year, providing full traceability for quality assurance and customer reporting.
Results
Our integrated solution transformed the client's ripening operations, delivering quantifiable improvements in product quality, operational efficiency, and supply chain reliability.
✔ Superior Product Quality The precision-controlled environment achieved excellent ripening uniformity across entire batches. Product rejection rates due to uneven ripening, color defects, or spoilage were reduced by over 65%, to a consistent rate below 3.5%.
✔ Significant Reduction in Product Loss By maintaining optimal and stable high humidity levels, the system drastically reduced dehydration and weight loss during the ripening process. Average weight loss was cut from over 5% to a consistent 1.8-2.2%, directly increasing salable yield and boosting profitability.
✔ Improve Operational Efficiency Full automation eliminated manual errors in gas handling and temperature control. The centralized system streamlined operations, allowing for better planning, reduced labor for monitoring, and improved on-time delivery performance to retailers. The client reported a 95% on-time delivery rate post-installation, up from approximately 80%.
 EN