EN

Cold storage control panels play a critical role in managing temperature and humidity levels for various storage applications, especially in the food, pharmaceutical, and logistics industries. As a purchasing manager or engineer, understanding the intricacies of these control panels is essential for ensuring the quality and efficiency of your cold storage systems. This article will help you evaluate the quality of cold storage control panels, guide you through the buying process, highlight common issues, and explain the cost factors involved.
A Buyeru2019s Guide
When purchasing a cold storage control panel, it is essential to have a clear understanding of your needs and the specifications that will meet them. Here are key considerations:
Application Requirements: Identify whether the panel will be used for food, pharmaceuticals, or logistics, as different applications may have differing regulatory requirements and performance expectations.
Technical Specifications: Prepare a detailed list of required specifications, including temperature range, control features, and energy efficiency ratings. This will facilitate accurate quotes from suppliers.
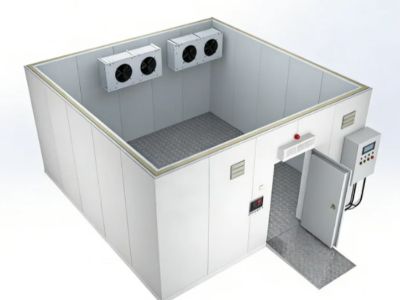
Customization Needs: Determine if you require custom solutions tailored to your specific application. Many manufacturers, including Shanghai Zhaoxue Refrigeration Co., Ltd., offer customization options to meet unique operational needs, such as Cold Room solutions.
Supplier Evaluation: Before making a purchase, assess potential suppliers based on their manufacturing capabilities, experience in the industry, and customer support services. Request references and case studies to gauge their reliability.
Request for Quotation (RFQ): When ready to proceed, prepare a comprehensive RFQ that includes your application details, quantity required, and any specific customization needs. This will help suppliers provide accurate pricing and lead times.
By following these guidelines, you can streamline the purchasing process and make informed decisions.