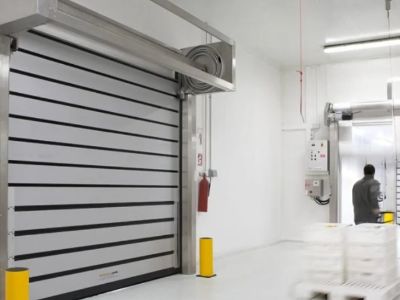
Custom Cold Room Solutions for Food and Pharma

Let's Discuss Your Needs

Every great collaboration starts with a friendly chat.
We're here to help you figure things out and find the best way forward.
Company Name
Name
Email
WhatsApp
Mobile

custom cold room

Custom cold rooms are specialized storage solutions designed to maintain precise temperature and humidity levels for various applications, including food preservation and pharmaceutical storage. When sourcing a custom cold room, B2B buyers often have concerns regarding quality, cost, application suitability, installation requirements, and the specific features that meet their operational needs. This article aims to provide insights into evaluating custom cold storage solutions, understanding cost factors, exploring applications in the food and pharma sectors, installation guidance, and identifying key features and benefits.

Cost Factors to Consider When Sourcing Custom Cold Rooms

Cost is a significant consideration when sourcing custom cold rooms. Various factors impact the overall pricing, including the room size, insulation thickness, and the complexity of the refrigeration system. Customization options—such as door configurations, shelving, and layout—also contribute to the final cost.

Additionally, energy efficiency is a crucial factor. Investing in high-efficiency compressors and insulation materials may result in higher upfront costs but can lead to substantial savings on energy bills over time. Buyers should request a detailed quotation that breaks down these components, allowing for better comparison between suppliers.

Another cost consideration is the total lifecycle cost, which includes maintenance and potential repair expenses. Understanding the manufacturer's warranty and support services can help mitigate unexpected costs in the future. Ensure to discuss lead times and delivery logistics, as these can also impact the overall budget.
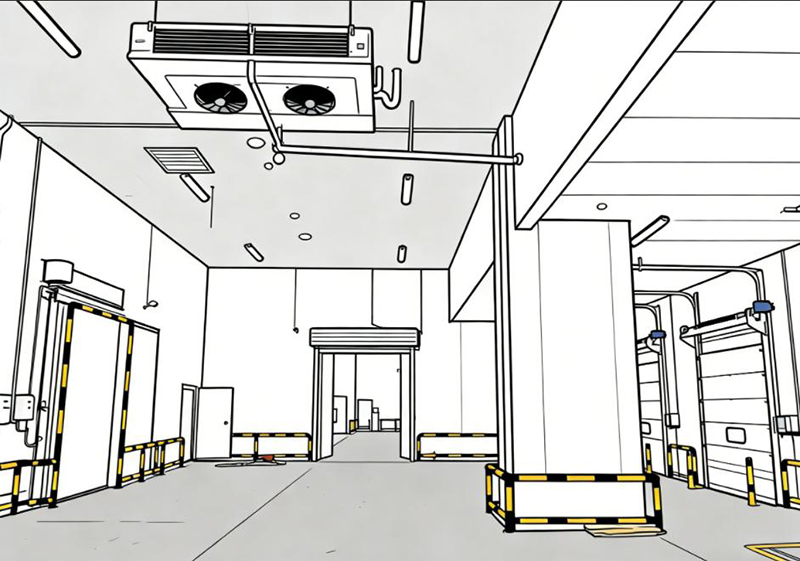
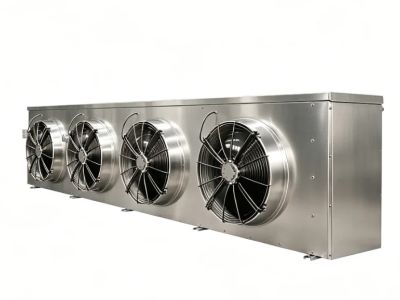
Applications of Custom Cold Rooms in Food and Pharma Industries

Custom cold rooms serve critical roles in both the food and pharmaceutical industries. In food storage, they are essential for preserving perishable goods, ensuring compliance with safety regulations, and extending shelf life. Different temperature ranges are required depending on the type of food—fresh produce, dairy, and meat all have specific storage needs that must be addressed during the design phase.

In the pharmaceutical sector, custom cold rooms are vital for storing temperature-sensitive medications and vaccines. The specifications for these rooms often include stricter temperature control and monitoring systems to ensure product efficacy and compliance with health regulations. Features like real-time temperature logging, alarm systems for deviations, and backup power options are common requirements.

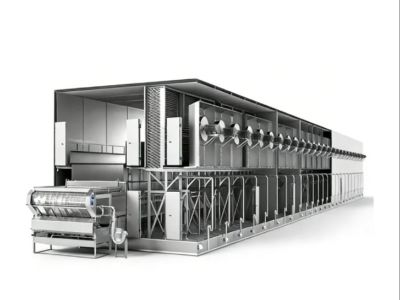
Understanding the specific application is critical when designing a custom cold room. Buyers should communicate their unique requirements, such as temperature ranges, humidity levels, and airflow needs, to ensure that the solution meets industry standards and operational needs. For instance, utilizing a Self-stacking Spiral Freezer can optimize storage for certain perishable items.

Installation Guidance for Custom Cold Room Systems

The installation of custom cold room systems involves several steps that require careful planning and execution. First, site evaluation is essential to determine the appropriate location, considering factors such as accessibility, utilities, and environmental conditions.

Next, a detailed installation plan should be developed, outlining the necessary resources, timelines, and personnel involved. Effective communication with the manufacturer can facilitate this process, ensuring that all dimensions and specifications are accurately adhered to.

During installation, it is crucial to follow the manufacturer's guidelines to avoid common pitfalls, such as improper sealing or inadequate insulation. After installation, a thorough inspection should be conducted to verify that all systems are functioning correctly.

Training for operational staff on proper usage and maintenance of the cold room is also essential to ensure optimal performance and longevity. Engaging with a manufacturer that provides installation support can enhance the success of the project.

Features and Benefits

Custom cold rooms come with a variety of features designed to enhance functionality and efficiency. Key features include advanced temperature control systems that allow for precise adjustments and monitoring. Some models incorporate smart technology, enabling remote access and alerts for temperature fluctuations or equipment malfunctions.

Energy efficiency features, such as LED lighting and high-performance insulation, help reduce operational costs. Additionally, options for modular designs allow for flexibility in space utilization, enabling businesses to adapt the room for different storage needs over time.

The benefits of investing in a custom cold room extend beyond mere storage. They include improved product quality through consistent environmental conditions, compliance with regulatory requirements, and enhanced operational efficiency. By choosing a reliable manufacturer like Shanghai Zhaoxue Refrigeration Co., Ltd., businesses can ensure they receive a solution tailored to their specific requirements, backed by expertise and quality assurance.

sourcing a custom cold room requires careful consideration of quality, cost, applications, installation, and features. By understanding these aspects, B2B buyers can make informed decisions that align with their operational goals.

How to Evaluate the Quality of Custom Cold Storage Solutions

When assessing the quality of custom cold storage solutions, several critical factors must be considered. Firstly, the materials used in construction play a significant role in insulation efficiency and durability. For instance, high-density polyurethane foam or extruded polystyrene is commonly utilized due to its excellent thermal properties. Buyers should verify the insulation thickness, as it directly affects energy consumption and temperature stability.

Another quality indicator is the manufacturer’s certifications, such as ISO standards, which reflect adherence to international quality management principles. Buyers should also inquire about the quality control processes in place, including any testing protocols for temperature uniformity and structural integrity. Understanding the production capabilities of the manufacturer—such as their machinery and technology—can also provide insights into the potential for customization and consistency in production quality.

Finally, it's beneficial to obtain references or case studies from previous customers to gauge satisfaction with performance and reliability. Engaging with a manufacturer like Shanghai Zhaoxue Refrigeration Co., Ltd., known for its energy-efficient solutions, can further ensure that the product meets industry standards.

Frequently Asked Questions

What is a custom cold room?

A custom cold room is a tailored refrigeration space designed to specific size, temperature, and workflow needs for food, pharma, or logistics applications.
We engineer rooms for a wide range: low-temperature freezers to chilled storage, typically from -40°C to +15°C depending on insulation and refrigeration choice.
Yes. We supply full services including site survey, custom design, installation, startup, and performance validation to ensure operational readiness.
Yes. We integrate automated controls, alarms, and remote monitoring options for temperature, humidity, and system status to meet operational and compliance needs.
We serve food, pharmaceutical, and logistics sectors, delivering energy-efficient designs and documentation to support regulatory and quality requirements.

Our Blog Posts

10 Fascinating Facts About Cold Room You Never Knew!

12

Oct

10 Fascinating Facts About Cold Room You Never Knew!

The World's Largest "Refrigerator" Can Hold the Entire City of Rome. The global cold storage network is vast beyond imagination. For instance, the total storage capacity of one of North America's largest cold storage operators exceeds 400 million cub...
View More
what does evaporator coil do

03

Nov

what does evaporator coil do

Understanding what an evaporator coil does is essential for anyone involved in the purchasing or maintenance of refrigeration systems. These coils play a crucial role in cooling processes by absorbing heat from the environment, making them indispensa...
View More
what are the methods of food preservation

03

Nov

what are the methods of food preservation

Food preservation is a critical process for maintaining the quality and safety of perishable items, especially in the food industry. Understanding what are the methods of food preservation can help businesses minimize waste, ensure product integrity,...
View More
what are the advantages of food preservation

03

Nov

what are the advantages of food preservation

Food preservation is a critical process that extends the shelf life of perishable goods such as fruits, vegetables, meats, and dairy products. Understanding the advantages of food preservation can greatly benefit businesses in the food industry, incl...
View More

Leave a Message

Email
Name
Company Name
Message
0/1000

Related product categories