Control Panel for Cold Room: Key Features and Suppliers

Let's Discuss Your Needs

Every great collaboration starts with a friendly chat.
We're here to help you figure things out and find the best way forward.
Company Name
Name
Email
WhatsApp
Mobile

control panel for cold room

A control panel for a cold room is a critical component that manages temperature and humidity levels to ensure optimal storage conditions for perishable goods. As a purchasing manager or engineer, you may face concerns regarding compatibility, efficiency, and reliability of control panels in cold storage applications. We will guide you through essential considerations when selecting a control panel for your cold room needs, including key specifications, reputable suppliers, quality evaluation processes, and diverse applications in various environments.

Key Specifications of Control Panels for Cold Storage Applications

When considering control panels for cold storage, several key specifications are crucial:

Temperature Range: Ensure the panel can operate within the specific temperature range required for your cold room, typically between -20°C and 10°C, depending on the stored products.

Control Type: Choose between digital or analog controls. Digital controls often provide more accurate readings and programmable settings.

Power Supply: Confirm that the power supply specifications match your facility's electrical system to avoid compatibility issues.

User Interface: A clear and intuitive user interface simplifies operation and reduces the likelihood of errors during adjustments.

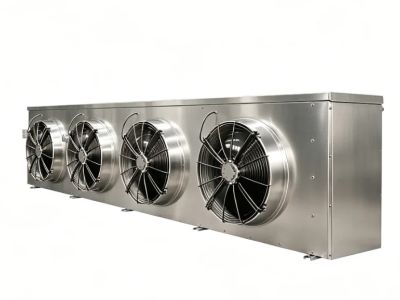
Connectivity: Look for control panels with communication capabilities, such as Modbus or Ethernet, for integration with building management systems (BMS) or remote monitoring. Additionally, consider how your control panel can work with various refrigeration units to enhance overall performance.

Understanding these specifications will help ensure that the control panel effectively meets your cold storage needs, minimizing risks of product spoilage and maximizing operational efficiency.
Reliable Suppliers of Cold Room Control Panels

Selecting a reputable supplier is essential for ensuring quality and reliability in your cold room control panel. When evaluating potential suppliers, consider their experience and expertise in manufacturing control panels for cold storage applications. Look for manufacturers that provide detailed product specifications and customization options to suit your specific requirements.

Shanghai Zhaoxue Refrigeration Co., Ltd. is known for its energy-efficient cold storage solutions, including custom-engineered control panels. Suppliers with a strong track record in the industry can offer valuable insights into product performance and reliability. Additionally, check for customer reviews and references to gauge the supplier's commitment to quality and service.

It’s advisable to request samples or demonstrations to assess product performance firsthand before making a bulk purchase. This can help you verify that the control panel meets your operational needs.

How to Evaluate Quality in Cold Room Control Panel Systems

Quality evaluation of cold room control panel systems involves several critical steps:

Material Selection: The materials used in the control panel construction should be durable and resistant to environmental factors typical in cold rooms, such as moisture and temperature fluctuations.

Testing Standards: Inquire about the testing standards the control panels adhere to. Look for compliance with industry standards, which can indicate reliability and safety.

Warranty and Support: A robust warranty and responsive customer support are essential indicators of quality. Suppliers that offer comprehensive support can help resolve issues quickly.

Performance Track Record: Review the performance history of the control panel in real-world applications. This can provide insights into its reliability and efficiency under various operating conditions.

Feedback from Existing Users: Consider reaching out to existing users of the control panel for their feedback regarding performance, maintenance, and any issues they may have encountered.

By following these evaluation steps, you can ensure that the control panel you choose is of high quality and suitable for your cold room applications.

Applications of Control Panels in Various Cold Room Environments

Control panels for cold rooms find applications across multiple industries, each with its specific requirements:

Food Storage: In food processing and storage facilities, control panels regulate temperature to ensure the safety and quality of perishable goods, extending shelf life and reducing waste.

Pharmaceuticals: Cold storage for pharmaceuticals requires precise temperature control to maintain the efficacy of medicines and vaccines. Control panels designed for this application often feature advanced monitoring and alarm systems.

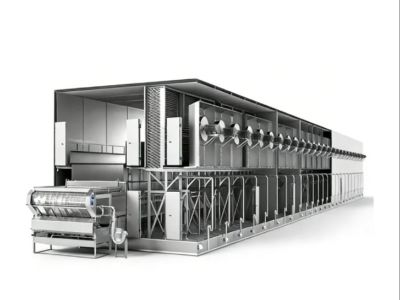
Logistics and Transportation: In logistics, control panels help manage temperature during the transport of temperature-sensitive goods. They ensure that the cold chain is maintained, which is critical for compliance and quality assurance. Utilizing efficient IQF freezers can also support maintaining the cold chain effectively.

Research Facilities: Laboratories often use cold rooms for sample storage. Control panels must offer precise control capabilities to meet the strict requirements of scientific research.

Understanding the specific applications of control panels will help you customize your solution to meet the unique demands of each environment, ensuring optimal performance and compliance with industry standards.

Choosing the Right Control Panel for Your Cold Room Needs

Selecting the right control panel for your cold room involves understanding your specific requirements, such as the type of goods being stored and the desired temperature range. A control panel should be compatible with your refrigeration system, whether it’s for a food processing facility, pharmaceutical storage, or logistics. When evaluating options, consider how well the panel integrates with existing machinery and its user interface's ease of use.

Additionally, the control panel should offer features like programmable temperature settings, alarms for temperature deviations, and data logging capabilities. These features enhance operational efficiency and allow for better monitoring of cold room conditions. Assessing the technical specifications, such as operating range, load capacity, and energy efficiency, will help you make an informed decision.

Our Blog Posts

how to set cold room temperature

03

Nov

how to set cold room temperature

Setting the right cold room temperature is crucial for industries that rely on precise temperature control to maintain the quality and safety of their products. Whether you are in the food, pharmaceutical, or logistics sector, understanding how to se...
View More
how to set temperature in chiller

03

Nov

how to set temperature in chiller

Setting the correct temperature in a chiller is crucial for maintaining the quality and safety of sensitive products, especially in industries like food, pharmaceuticals, and logistics. This article will address key considerations for B2B buyers, inc...
View More
what does evaporator coil do

03

Nov

what does evaporator coil do

Understanding what an evaporator coil does is essential for anyone involved in the purchasing or maintenance of refrigeration systems. These coils play a crucial role in cooling processes by absorbing heat from the environment, making them indispensa...
View More
what are the advantages of food preservation

03

Nov

what are the advantages of food preservation

Food preservation is a critical process that extends the shelf life of perishable goods such as fruits, vegetables, meats, and dairy products. Understanding the advantages of food preservation can greatly benefit businesses in the food industry, incl...
View More

Leave a Message

Email
Name
Company Name
Message
0/1000

Related product categories